

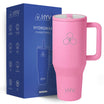
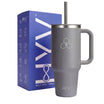
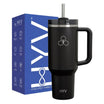
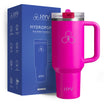
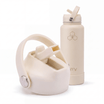
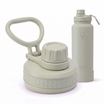


A multi-part lid needs a separate mould for every moulded component, so "tooling a lid" is rarely one tool — a sipper lid with a shell, a catch, a spout insert and a silicone gasket is four tools in three materials. Cavitation then sets your economics: a single-cavity tool is cheap to make and slow to run, a multi-cavity tool is the reverse, and the choice fixes your per-unit cost for the life of the product. This is why tooling a lid only pays back when the mechanism itself is the reason customers buy, and why most brands are better served adapting an existing lid.
Key Facts
- Every moulded part needs its own tool. A multi-part lid is several moulds.
- Silicone gaskets are compression moulded — a different tool and a different process.
- Cavitation trades tool cost against cycle time, and the choice is permanent.
- Tooling a lid pays back only when the mechanism is the purchase reason.
- Adapting an existing lid — colour, branding, straw, gasket spec — needs no tooling.
Our pick on this page: Luxe Sipper Lid, ₹299. Full reasoning below.
Counting the tools honestly
Take a flip-top sipper and list what has to be moulded: the outer shell, the flip cap, a locking catch if it is separate, a spout insert, and the gasket. That is four injection tools and one compression tool, in at least two materials.
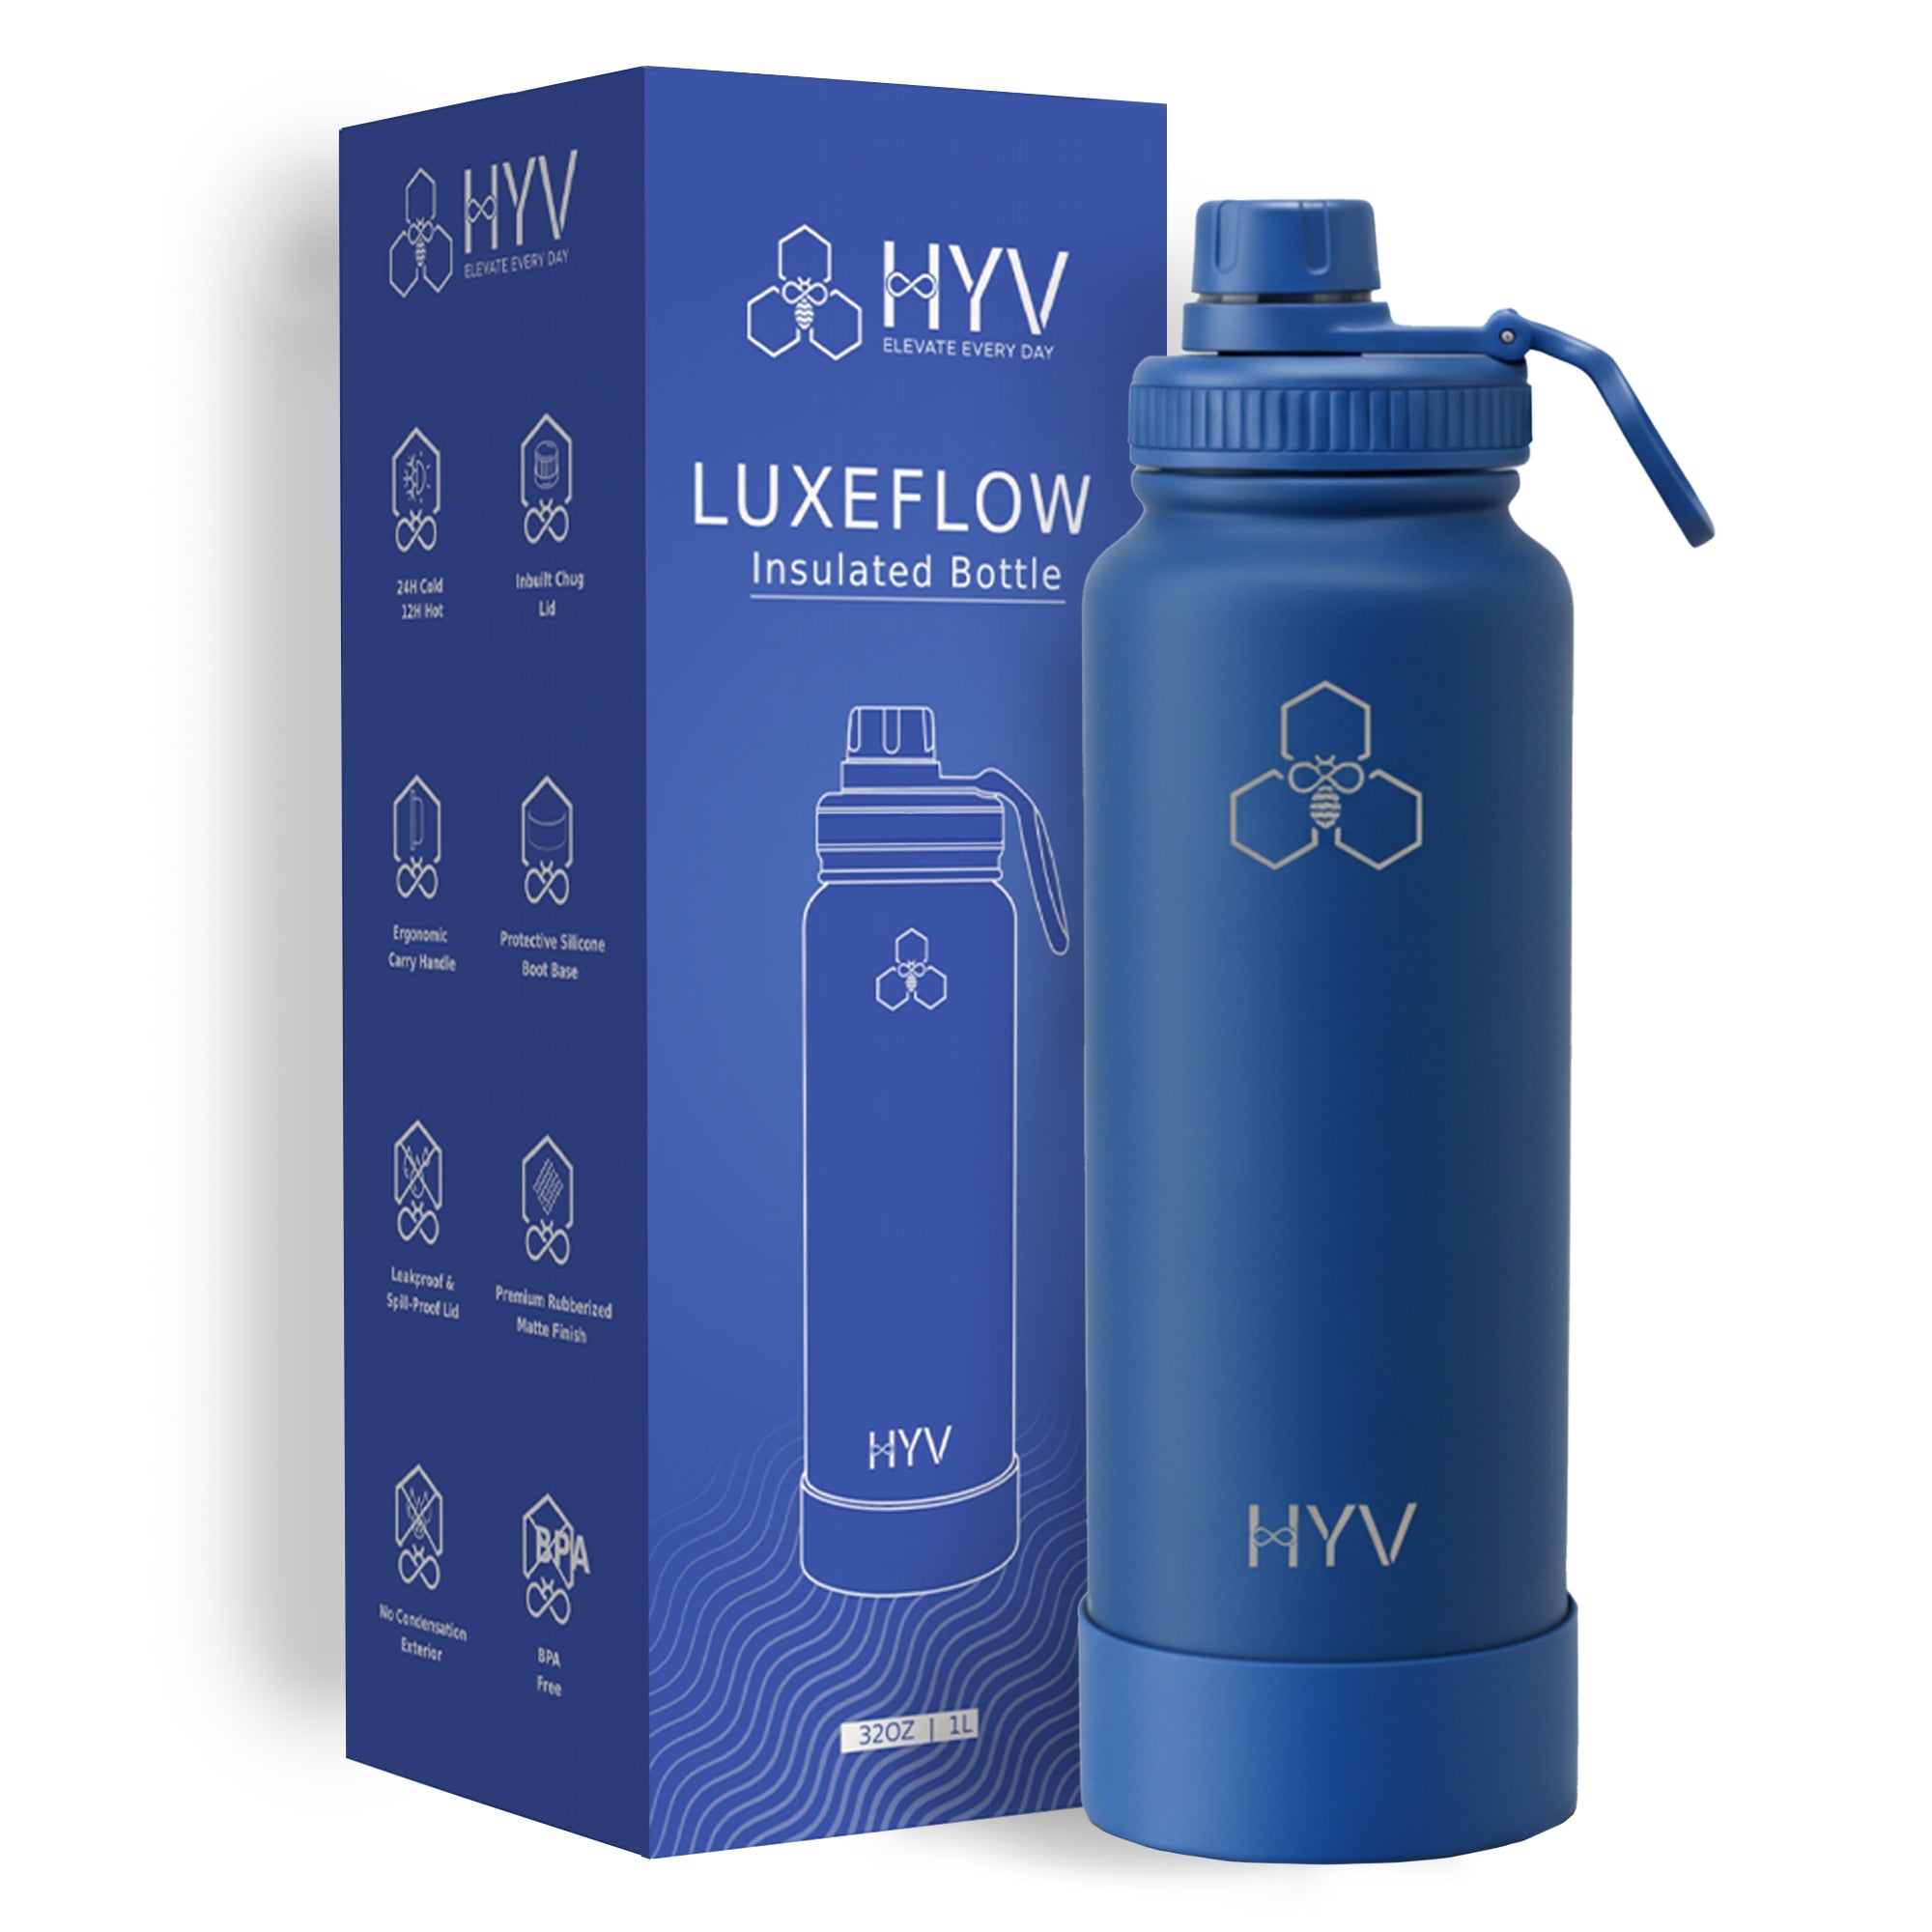
A magnetic chug lid substitutes a magnet housing for the catch, which is another injection tool plus a bought-in magnet with its own supply and quality variance. A 2-in-1 lid that offers both chug and sipper modes needs the parts for both plus the mechanism that switches between them.
So when a supplier quotes "lid tooling", the first question is how many tools, for which parts, and which parts are bought in rather than tooled. A low tooling quote usually means most of the lid is somebody else's existing part — which may be perfectly good, and is a different proposition from owning the design.
Cavitation, and the decision you cannot revisit
A mould can produce one part per cycle or many. A 2-cavity tool costs less to cut and produces half as fast as a 4-cavity. The tool cost and the per-unit cost trade directly against each other.
The decision is effectively permanent, because re-cutting a tool to add cavities is close to making a new one. So it has to be made against a volume forecast, and a brand that tools for optimism carries the cost of capacity it never uses while one that tools conservatively hits a unit-cost ceiling just as the product works.
The practical guidance: if you cannot forecast volume to within a factor of two, you are not ready to tool. Run on an existing lid, learn the real demand, and tool against evidence.
What you can change without any tooling at all

More than brands expect, and this is the route most should take:
- Colour. A coating or a masterbatch change, not a tool. At HYV a dedicated colourway starts at 1,000 units.
- Branding. Laser etching or UV printing on the lid or body. From 25 units per SKU.
- Straw. Extruded, so length and material are variable without new moulds.
- Gasket specification. A different hardness from the same tool, if the supplier's gasket source offers it.
- Which lid goes on which body. Free, where the necks are shared — and the highest-leverage option of the five.
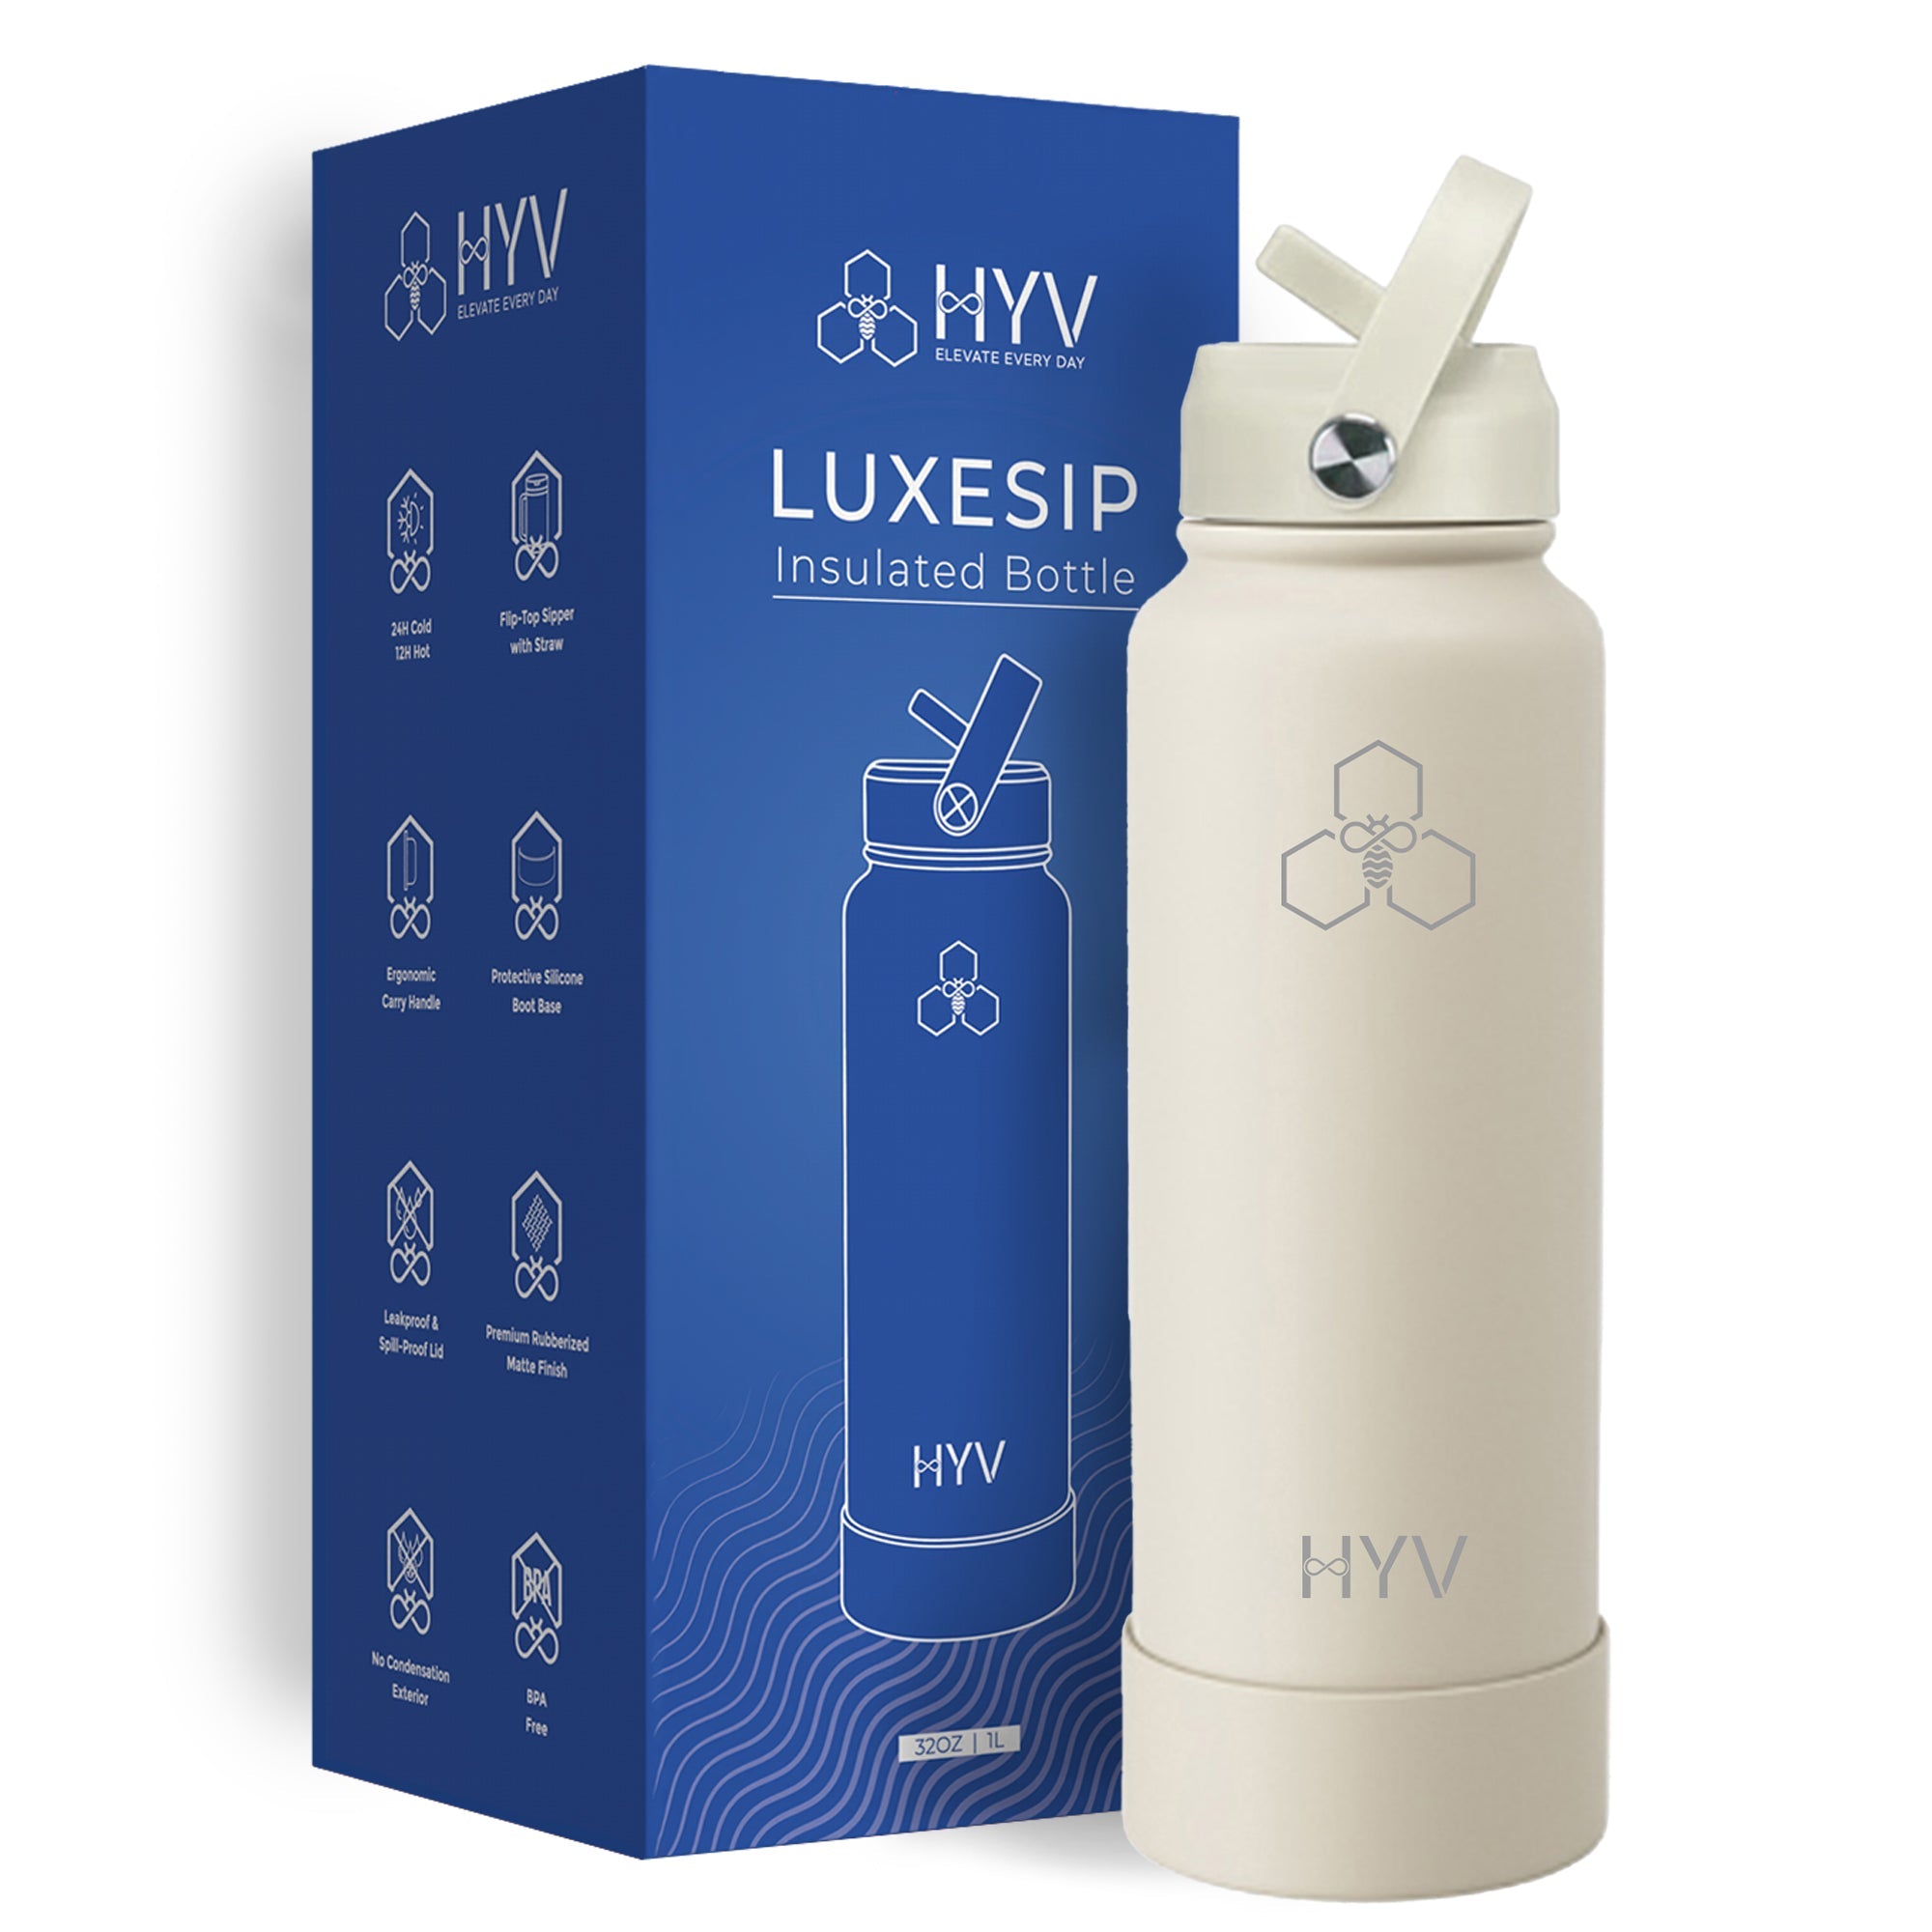
HYV's one-litre bodies share a neck, so the flip-top sipper at ₹299, the wide-mouth chug at ₹299 and the magnetic chug at ₹399 all fit all three. A 25-unit order can therefore ship as three distinct products with no tooling and no new parts.
The body is the more expensive half of the same question: what body tooling costs you, as against lid tooling.
Disclosure
HYV does not cut tooling for outside designs, so a page arguing that most brands should not tool a lid is plainly in its interest. The counter-case is real and worth stating: if your product's reason to exist is a mechanism nobody else sells, an existing lid cannot deliver it and tooling is the only route. Where HYV is not the answer: exactly that case. HYV makes insulated steel bottles from ₹899.
Related reading: writing a bottle design brief for a manufacturer and oem water bottle manufacturer what oem actually means.
Frequently Asked Questions
How many moulds does a lid need?
One per moulded part. A typical sipper lid is four injection tools plus a compression tool for the gasket. Ask a supplier to itemise which parts are tooled and which are bought in.
What is cavitation and why does it matter?
How many parts a mould makes per cycle. More cavities cost more to cut and produce faster, so the choice fixes your per-unit cost for the product's life and is not practically reversible.
Can I tool just the shell and buy the rest?
Often yes, and it is a sensible middle route — you own the visible part and use proven internals. Be clear in the agreement about who owns which tool and who may use it.
When is tooling a lid worth it?
When the mechanism is the reason people buy, and when you can forecast volume to within a factor of two. If your differentiator is colour, logo or bundle, tooling buys something the customer cannot see.
What can I change without tooling?
Colour, branding, straw, gasket specification, and which lid pairs with which body where necks are shared. That last one costs nothing and does the most.
Trade enquiry
HYV manufactures its own lids — sipper, chug, magnetic, 2-in-1, straw and steel screw-top — and contract-manufactures insulated steel drinkware under other brands. Tell us the mechanism and the quantity.
Send a manufacturing brief →Minimum 25 units per SKU · custom colourway from 1,000 · 7–14 days from a confirmed brief · UV print or laser etching


Leave a comment
This site is protected by hCaptcha and the hCaptcha Privacy Policy and Terms of Service apply.